

Introduction to Desulfurization Sodium Bicarbonate Pneumatic Conveying Equipment: Structure and Work
Desulfurization sodium bicarbonate pneumatic conveying equipment is a specialized industrial device designed for the efficient and safe transportation of sodium bicarbonate, a key chemical used in flue gas desulfurization processes. This equipment plays a crucial role in modern industrial applications, particularly in power plants and chemical facilities where precise handling of desulfurization reagents is essential for environmental compliance and operational efficiency.
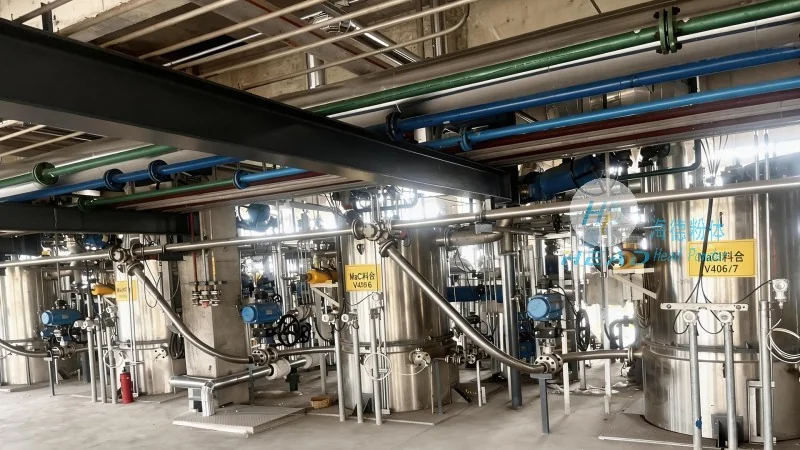
Overview of the Desulfurization Sodium Bicarbonate Pneumatic Conveying Equipment
The desulfurization sodium bicarbonate pneumatic conveying equipment is engineered to handle the transportation of sodium bicarbonate from storage silos or reactors to the point of use in flue gas desulfurization systems. It operates on the principle of pneumatic conveying, which uses compressed air or other gas to move bulk materials through a pipeline system. This method offers several advantages over traditional mechanical conveying systems, including reduced equipment wear, lower maintenance costs, and the ability to transport materials over longer distances without the need for multiple transfer points.
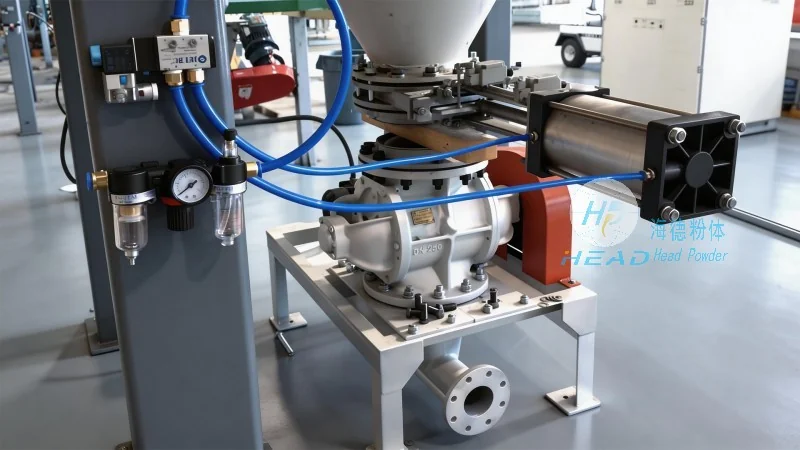
Key Structural Components and Working Principle
The equipment consists of several core components that work in tandem to ensure reliable operation. The main parts include a material feeder, a conveying pipeline, a pressure vessel or receiver, a control system, and an air supply unit. The material feeder is responsible for feeding the sodium bicarbonate into the conveying system, ensuring a consistent flow rate. The conveying pipeline, typically made of corrosion-resistant materials such as stainless steel or special alloys, transports the material under pressure. The pressure vessel or receiver collects the material at the destination and may include a discharge mechanism to release the material into the desulfurization system. The control system monitors and regulates the air pressure, flow rate, and material feed, ensuring optimal performance and preventing overpressure or underflow conditions. The air supply unit provides the necessary compressed air or gas to generate the conveying force.
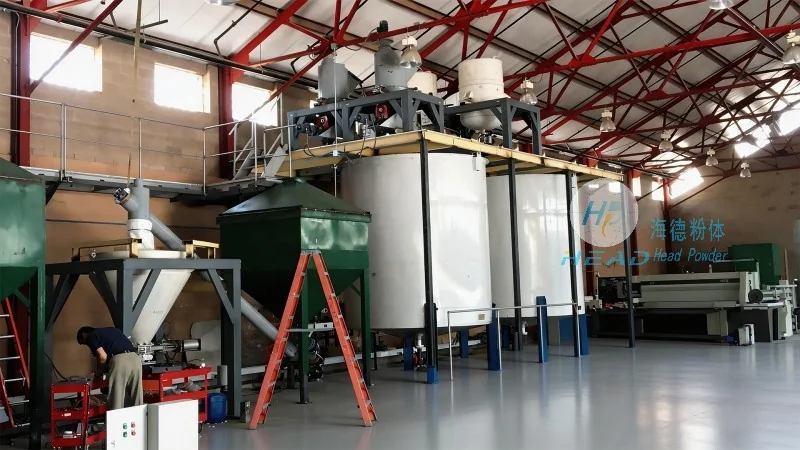
Advantages of Using Pneumatic Conveying for Desulfurization Applications
Implementing pneumatic conveying for sodium bicarbonate in flue gas desulfurization processes offers numerous benefits. Firstly, it minimizes material degradation and contamination, as the material is enclosed within the pipeline, protecting it from moisture, dust, and other environmental factors. Secondly, it enhances safety by reducing the risk of dust explosions and material spillage, which are common hazards in traditional handling methods. Thirdly, the system allows for precise control over the material flow rate, ensuring consistent dosing in the desulfurization process, which is critical for maintaining optimal pH levels and sulfur removal efficiency. Additionally, pneumatic conveying systems are more compact and require less floor space compared to mechanical conveyors, making them suitable for installations with limited space. The equipment also offers flexibility in terms of layout, as the pipeline can be routed around obstacles and adapted to different plant configurations.
Application in Flue Gas Desulfurization Systems
In flue gas desulfurization (FGD) systems, sodium bicarbonate is used as a reagent to neutralize sulfur dioxide (SO2) in the exhaust gases from coal-fired power plants. The pneumatic conveying equipment ensures that the sodium bicarbonate is delivered to the absorber or reaction tower at the correct concentration and flow rate. This consistent supply is vital for maintaining the efficiency of the FGD process, as any fluctuations in the reagent feed can lead to reduced sulfur removal rates or increased corrosion in the system. The equipment's ability to handle the bulk material in a controlled manner helps in achieving stable operation and minimizing downtime, which is crucial for power plant productivity and environmental compliance.
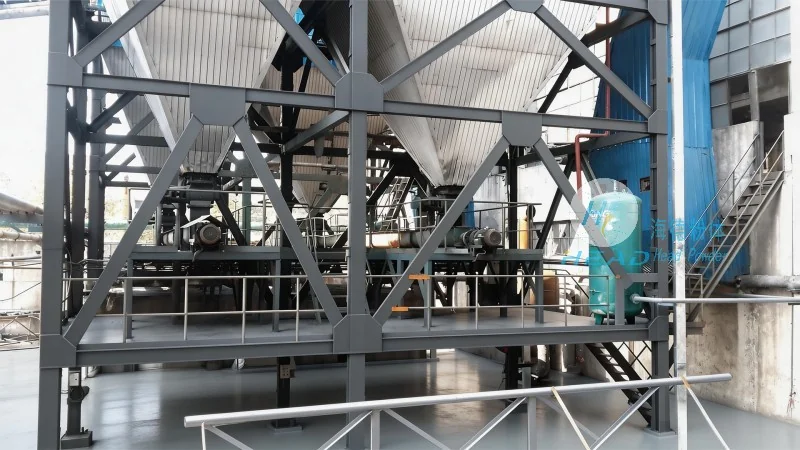
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of industrial conveying equipment, including desulfurization sodium bicarbonate pneumatic conveying systems. The company is headquartered in Shandong, China, and has established a strong reputation for producing high-quality, reliable equipment tailored to the needs of various industrial sectors. With a focus on innovation and customer satisfaction, headpowder utilizes advanced engineering techniques and rigorous quality control processes to ensure that its products meet international standards and deliver long-term performance. The company's expertise in pneumatic conveying technology and desulfurization applications enables it to provide comprehensive solutions that enhance operational efficiency and environmental performance for its clients.