

Analysis of Gray Calcium Pneumatic Conveying Systems
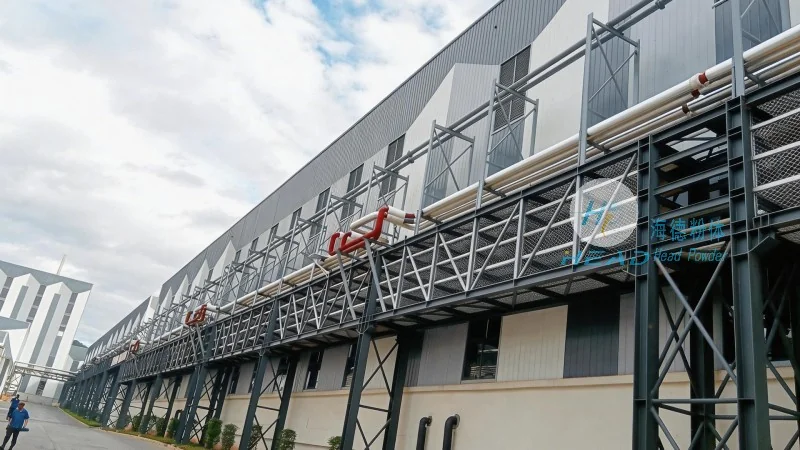
Gray calcium, also known as calcium hydroxide, is a widely utilized industrial material across sectors like construction, agriculture, and chemical manufacturing. The efficient and reliable transportation of gray calcium from production sites to processing or storage facilities is critical for maintaining production efficiency and ensuring product quality. Pneumatic conveying systems have become a preferred solution for handling this material due to their ability to transport bulk materials in a dust-free, controlled environment. This article provides an in-depth analysis of a specialized gray calcium pneumatic conveying system designed and manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading company in powder handling technology.
Introduction to Gray Calcium and Pneumatic Conveying
Gray calcium, chemically calcium hydroxide (Ca(OH)₂), is a fine powder with a Mohs hardness of 1.5. It is commonly used as a building material, in cement production, as a soil conditioner, and in water treatment. Due to its fine particle size and hygroscopic nature, traditional handling methods like belt conveyors or bucket elevators can cause dust generation, material degradation, and operational inefficiencies. Pneumatic conveying systems offer a solution by using air pressure to move material through a pipeline network, minimizing external contact and reducing contamination risks.
Key Features of the HeadPowder Gray Calcium Pneumatic Conveying System
The gray calcium pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is engineered to address the unique challenges of handling calcium hydroxide. The system incorporates advanced features that enhance performance and reliability. Firstly, it includes a high-efficiency dust collection and filtration system to ensure material is conveyed in a clean, dust-free manner, critical for product purity and compliance with environmental regulations. The system also uses a variable frequency drive (VFD) for the air compressor, enabling precise control of air pressure and flow rate to optimize energy use and reduce costs.
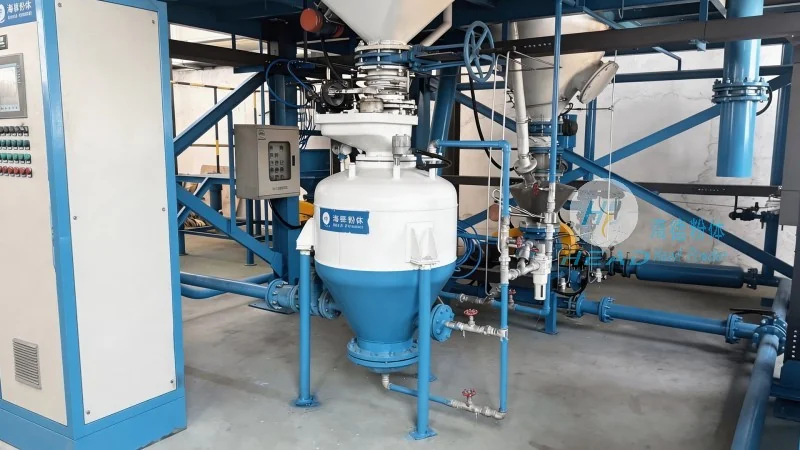
Another key feature is the use of corrosion-resistant materials for pipelines and components. The system employs stainless steel or specialized alloys to withstand the material's corrosive properties, ensuring long-term durability and low maintenance. Additionally, a real-time monitoring and control panel provides operators with immediate feedback on system performance (air pressure, flow rate, material levels), allowing quick adjustments and proactive maintenance to enhance reliability.
Advantages of the Pneumatic Conveying System for Gray Calcium
The pneumatic conveying system offers several advantages over traditional methods. Primary benefits include reduced dust generation, improving workplace safety and preventing product contamination. The closed pipeline system minimizes material loss and improves recovery rates. Controlled handling also maintains moisture content and prevents caking or agglomeration that can occur with open systems.
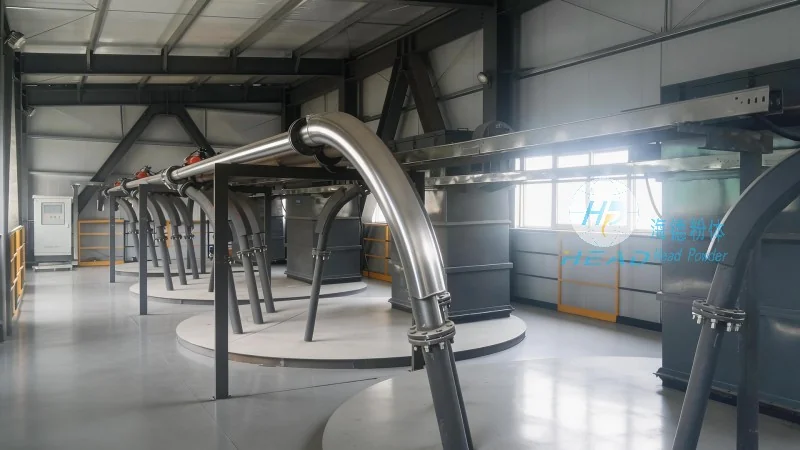
Operationally, the system provides flexibility in material routing, easily integrating with existing production lines and reconfigurable for changing needs. Its compact design suits both new and retrofit installations. Energy efficiency, especially with VFD-controlled compressors, lowers operational costs and environmental impact.
Application Scenarios and Performance Metrics
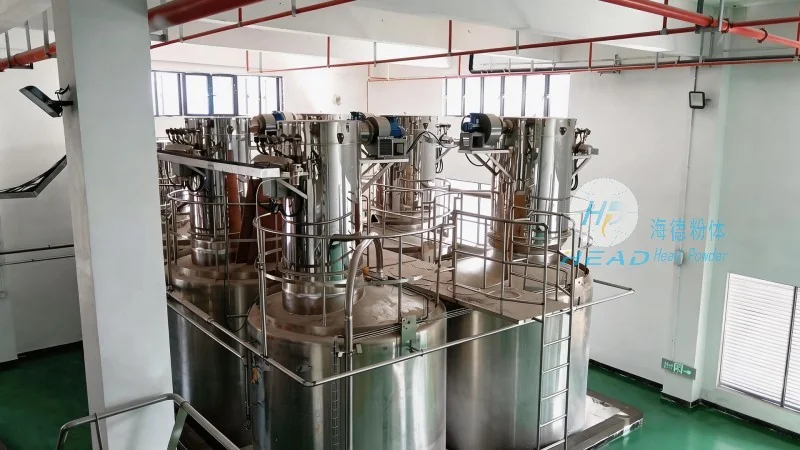
The system is suitable for transporting raw gray calcium from silos to production lines, finished products to packaging facilities, or waste for recycling. Typical flow rates range from 1 to 50 tons per hour, depending on configuration and pipeline length. Performance metrics show high efficiency: material recovery rates over 99% and significantly lower dust emissions than open conveyors.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in advanced powder handling systems. The company’s expertise in pneumatic conveying, combined with quality commitment, makes its gray calcium system a preferred choice for industries needing reliable material transport. By leveraging technology and adhering to standards, HeadPowder delivers robust solutions for modern industrial operations. For businesses seeking to improve gray calcium handling, the HeadPowder system represents a cost-effective, efficient option.