

Introduction to Lithium Hydroxide Conveying Systems and the Advantages of Air-Driven Lithium Hydroxi
HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced conveying systems designed for the efficient and safe transportation of lithium hydroxide. This article provides an in-depth look at lithium hydroxide conveying systems, with a focus on the benefits and features of air-driven conveying technology.
Overview of Lithium Hydroxide Conveying Systems
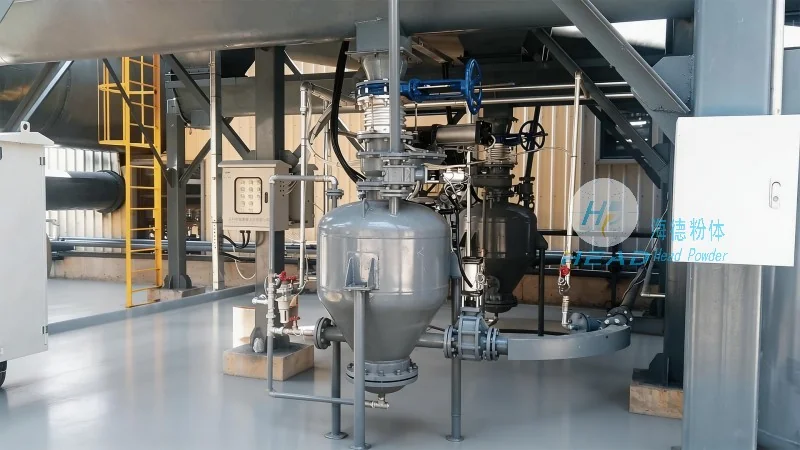
Lithium hydroxide (LiOH) is a critical chemical compound widely used in various industries, including battery manufacturing, chemical production, and as a precursor in pharmaceuticals. The safe and efficient transportation of LiOH is essential to maintain production efficiency and ensure product quality. Conveying systems for lithium hydroxide must address specific challenges such as material handling, dust control, and environmental safety. HeadPowder's lithium hydroxide conveying systems are engineered to meet these demands, offering reliable and high-performance solutions tailored to industrial needs.
Advantages of Air-Driven Conveying for Lithium Hydroxide
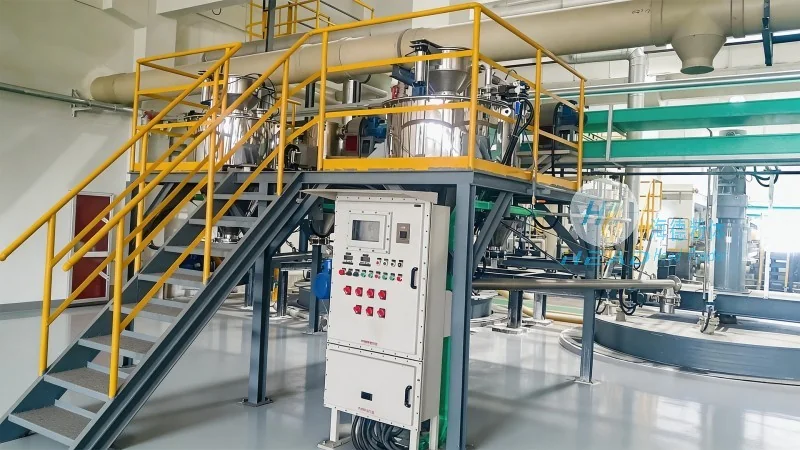
One of the most effective methods for transporting lithium hydroxide is through air-driven conveying, also known as pneumatic conveying. This technology utilizes compressed air to move the material through a pipeline system, eliminating the need for mechanical components like belts or buckets. The advantages of air-driven conveying for lithium hydroxide are numerous and significant. Firstly, it provides a dust-free and enclosed environment, which is crucial for maintaining product purity and preventing contamination. Secondly, the system offers high flexibility in terms of layout and installation, allowing for complex routing and integration with existing production lines. Thirdly, air-driven conveying can handle a wide range of material characteristics, including fine powders and granules, with minimal degradation. Additionally, this method reduces mechanical wear and tear, leading to lower maintenance costs and longer system lifespan. For industries dealing with lithium hydroxide, these benefits translate into improved operational efficiency, enhanced safety, and reduced environmental impact.
Key Features of HeadPowder's Lithium Hydroxide Conveying Solutions
HeadPowder Engineering Co., Ltd., based in Shandong, China, is dedicated to delivering top-tier conveying solutions for lithium hydroxide. Our systems are designed with several key features that set them apart in the market. The use of high-quality materials ensures durability and resistance to corrosion, which is vital for handling chemical substances like lithium hydroxide. Advanced control systems allow for precise regulation of air pressure and flow, optimizing the conveying process and minimizing energy consumption. The enclosed and sealed design of our conveying lines prevents dust emissions and ensures compliance with environmental regulations. Furthermore, our solutions are scalable, enabling businesses to expand their operations without the need for major system overhauls. HeadPowder's commitment to innovation and customer satisfaction has made us a trusted partner for companies seeking reliable lithium hydroxide conveying systems.
Conclusion and Application Scope
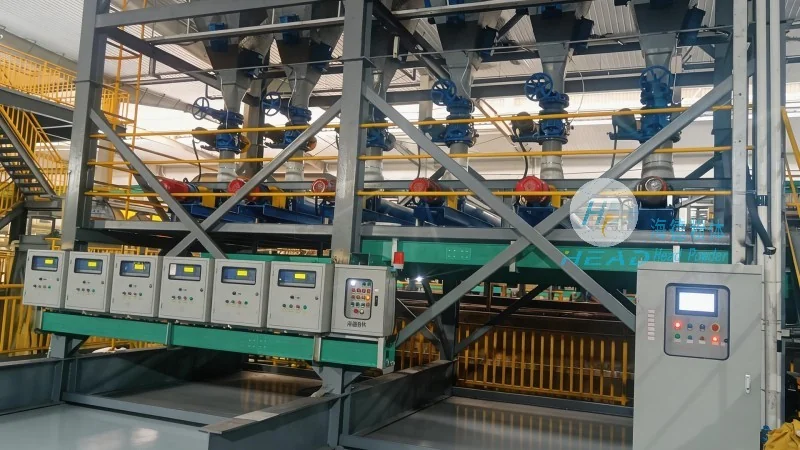
In conclusion, the introduction of advanced lithium hydroxide conveying systems, particularly those utilizing air-driven technology, has revolutionized the way industries handle this critical chemical. The advantages of such systems, including dust control, flexibility, and efficiency, make them indispensable in modern production environments. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, continues to lead the way in providing cutting-edge conveying solutions that meet the evolving needs of the industry. By leveraging the benefits of air-driven conveying, companies can enhance their operational performance, ensure product safety, and maintain a competitive edge in the market.