

Types, Features, and Applications of Calcite Pneumatic Conveying Systems
Calcite, a common calcium carbonate mineral, is widely used in various industries such as construction, pharmaceuticals, and chemical manufacturing. The efficient transportation of calcite powder through pneumatic conveying systems is crucial for maintaining production efficiency and product quality. This article explores the types, key features, and application ranges of calcite pneumatic conveying systems, highlighting the technical advancements and practical benefits offered by these systems.
Types of Calcite Pneumatic Conveying Systems
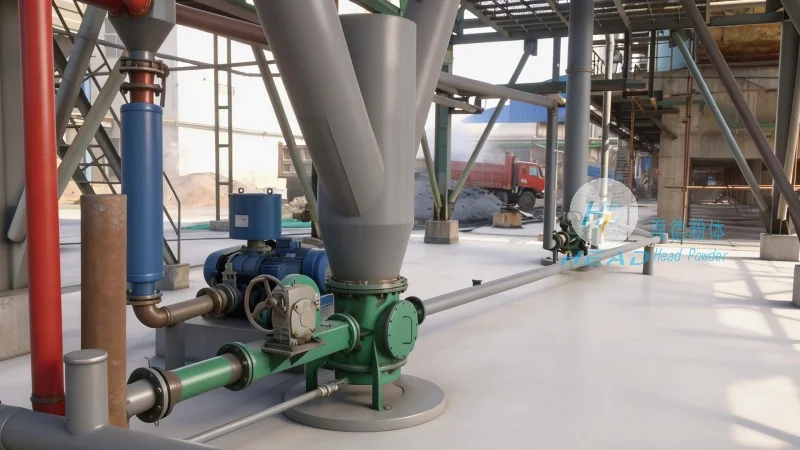
There are primarily two main types of pneumatic conveying systems used for calcite powder: positive pressure systems and negative pressure systems. Positive pressure systems operate by blowing air or gas into the conveying line, pushing the material forward. This method is suitable for short to medium distances and is commonly used in industries where dust control is a priority. Negative pressure systems, on the other hand, create a vacuum in the conveying line, drawing the material from the source. These systems are ideal for long-distance conveying and are often used in applications where material is to be transported from multiple points to a central collection point.
Key Features of Calcite Pneumatic Conveying Systems
Calcite pneumatic conveying systems are designed with several key features that enhance their performance and reliability. One of the primary features is the ability to handle fine powders without causing excessive wear to the system components. This is achieved through the use of specialized materials and components that are resistant to abrasion and corrosion. Another important feature is the system's flexibility in terms of layout and integration with existing production lines. This allows for easy installation and adaptation to different production environments.
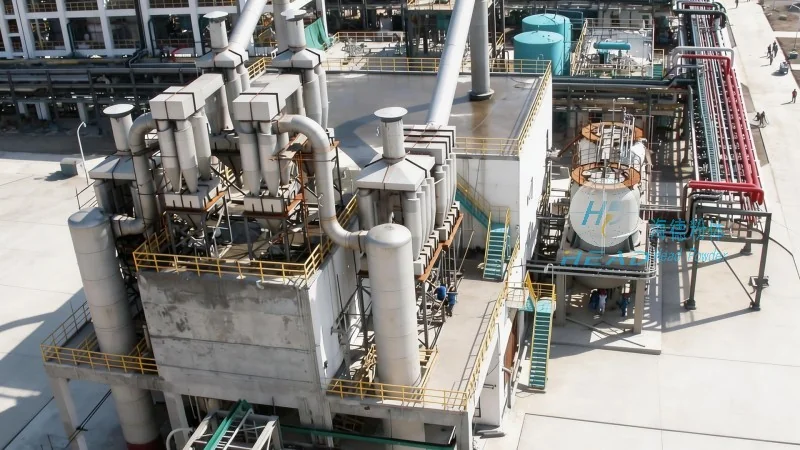
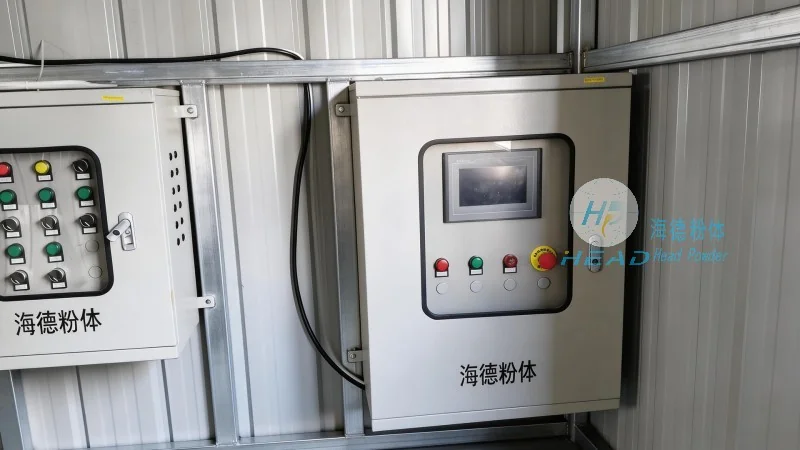
Additionally, modern calcite pneumatic conveying systems incorporate advanced control systems that monitor and regulate the flow of material and air. These systems can detect blockages, adjust pressure, and maintain consistent conveying rates, ensuring smooth and continuous operation. The use of high-quality materials and precision engineering also contributes to the long service life and low maintenance requirements of these systems.
Application Ranges of Calcite Pneumatic Conveying Systems
The application ranges of calcite pneumatic conveying systems are extensive, covering a wide range of industries and processes. In the construction industry, calcite is used as a filler in cement and concrete, and pneumatic conveying systems are used to transport calcite powder from storage silos to mixing plants. In the pharmaceutical industry, calcite is used as an excipient in tablets and capsules, and the systems ensure that the powder is transported hygienically and without contamination.
In the chemical industry, calcite is used in the production of calcium carbonate products, and pneumatic conveying systems are used to transport raw materials and finished products between different processing stages. The systems are also used in the food industry for the transportation of calcium carbonate used as a food additive. The versatility of calcite pneumatic conveying systems makes them suitable for various applications, from small-scale laboratory use to large-scale industrial production.
Company Information and Expertise
Shandong HeadPowder Engineering Co., Ltd., a leading provider of calcite processing and conveying solutions, specializes in the design, manufacturing, and installation of pneumatic conveying systems. With years of experience in the industry, the company has developed a deep understanding of the unique challenges associated with calcite powder handling. The company's team of engineers and technicians work closely with clients to provide customized solutions that meet their specific production requirements.
HeadPowder's calcite pneumatic conveying systems are designed to be efficient, reliable, and cost-effective. The company uses advanced technology and high-quality materials to ensure that its systems meet the highest standards of performance and safety. The company's commitment to quality and customer satisfaction has earned it a reputation as a trusted partner in the industry.