

Components of Bulk Barley Pneumatic Conveying
When considering the components of bulk barley pneumatic conveying systems, it's essential to understand the integrated elements that ensure efficient and reliable material handling. These systems are critical in industries dealing with grain and agricultural products, particularly for barley, which requires specialized equipment to maintain quality and operational efficiency.
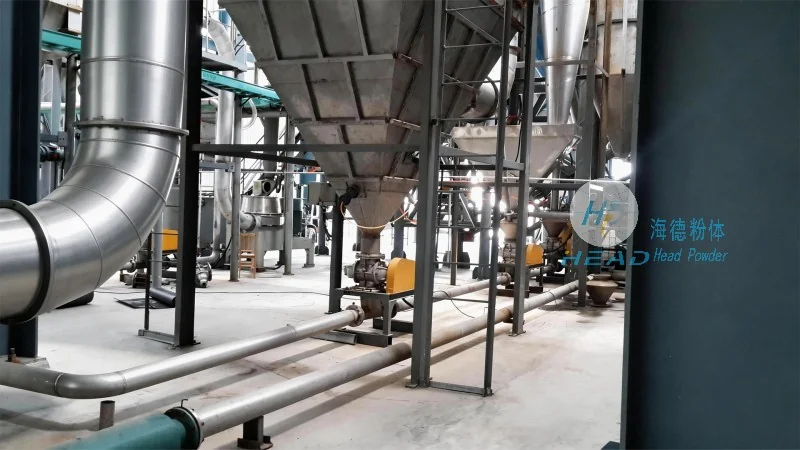
Key Components of Bulk Barley Pneumatic Conveying
The core components of a bulk barley pneumatic conveying system typically include several key elements designed to handle the unique characteristics of barley. These components work in tandem to facilitate the movement of barley from storage to processing areas. The primary components are as follows:
1. Hopper and Feeder System
The hopper and feeder system is the initial component that manages the flow of barley from storage bins or silos. This system ensures a consistent and controlled feed rate, preventing overloading or underfeeding that could disrupt the conveying process. The hopper is designed to accommodate the bulk volume of barley, while the feeder, often a rotary or vibratory type, regulates the material's discharge into the conveying line. This component is crucial for maintaining the uniformity of the material flow, which is vital for preventing blockages and ensuring the longevity of downstream equipment.
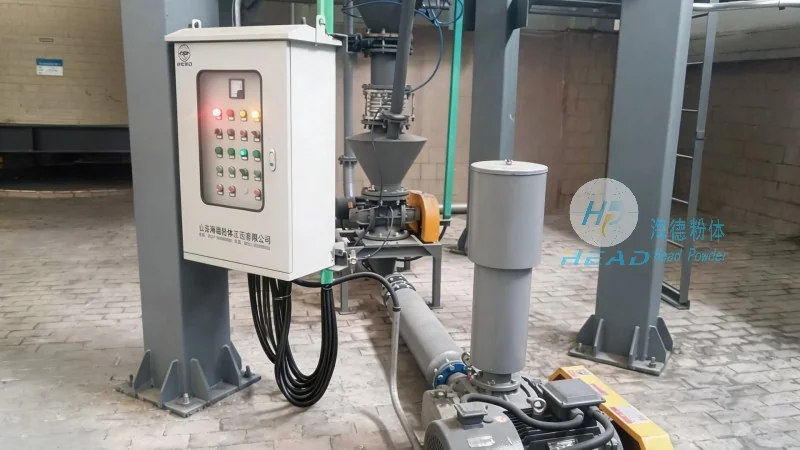
2. Conveying Line and Air Supply
The conveying line, which can be made of stainless steel or other corrosion-resistant materials, is the main pathway for transporting barley. This line is connected to a high-pressure air supply system, which provides the necessary force to move the barley particles through the pipeline. The air supply system typically includes a blower or compressor that generates the required air pressure, often ranging from 5 to 15 bar depending on the system's capacity and the distance the barley needs to travel. The design of the conveying line, including bends and transitions, is optimized to minimize pressure loss and maintain the air flow efficiency, ensuring that the barley moves smoothly without excessive energy consumption.
3. Separation and Cleaning Equipment
After the barley reaches its destination, separation and cleaning equipment are essential to remove any excess air and separate the barley from the conveying medium. This may include cyclone separators, filters, or rotary air locks. These components help maintain the purity of the barley and prevent contamination from dust or other particles. The separation process is critical for maintaining the quality of the barley, which is important for subsequent processing steps such as malting or milling. The equipment is designed to handle the abrasive nature of barley and ensure long-term operational reliability.
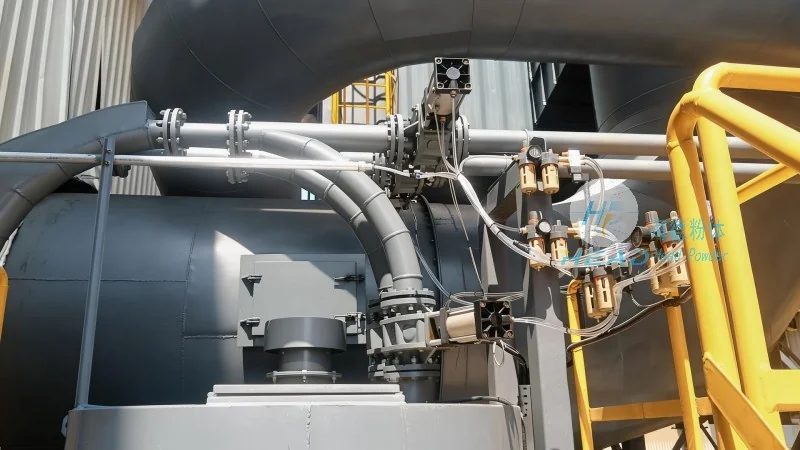
4. Control and Monitoring Systems
Modern bulk barley pneumatic conveying systems are equipped with advanced control and monitoring systems to optimize performance and ensure safety. These systems include sensors for measuring air pressure, flow rates, and material levels, as well as control panels that allow operators to adjust the system parameters in real-time. The monitoring systems help detect any anomalies or inefficiencies, such as blockages or pressure drops, allowing for immediate intervention. This not only improves operational efficiency but also reduces downtime and maintenance costs. The control systems are typically integrated with the other components, creating a cohesive and automated operation.
About HeadPowder Engineering
HeadPowder Engineering, a leading provider of bulk material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of the grain and agricultural industries. With a focus on quality and innovation, HeadPowder offers customized solutions that meet the specific requirements of barley processing facilities. The company is headquartered in Shandong, China, and serves clients globally with expertise in material handling technology. HeadPowder's commitment to excellence ensures that their systems are reliable, efficient, and durable, providing long-term value to their customers.