

Working Principle and Features of Metering Bin Pump Pneumatic Conveying Equipment
For industrial applications requiring efficient and reliable material handling, the metering bin pump plays a crucial role in pneumatic conveying systems. This equipment is designed to transport bulk materials such as powders, granules, and other particulate substances through a pressurized air system. Understanding its working principle and key features is essential for selecting the right solution for specific operational needs.
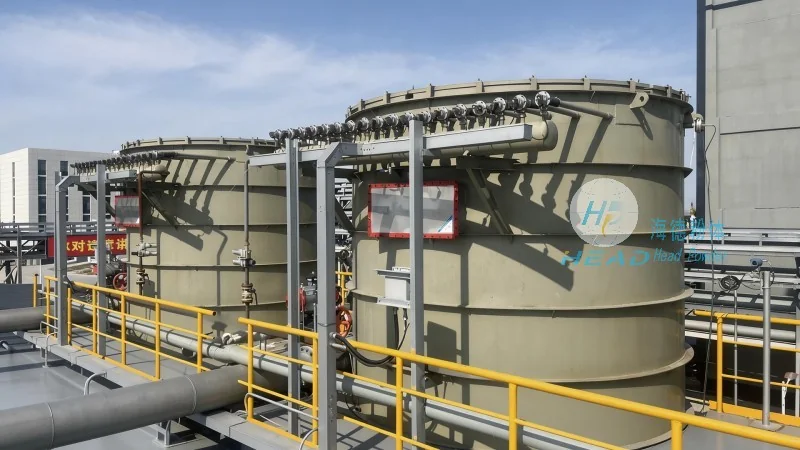
Working Principle of Metering Bin Pump Pneumatic Conveying Equipment
The core operation of a metering bin pump involves the controlled feeding of material from a storage bin into a conveying line using compressed air. The process typically begins with the material being stored in a hopper or bin, where it is held under a slight pressure to prevent clogging and ensure consistent flow. As the conveying system requires material, the bin pump's valve opens, allowing a measured amount of material to be discharged into the air stream. The compressed air then propels the material through the pipeline to the destination point, such as a silo, storage tank, or processing unit. This method eliminates the need for mechanical components like screws or belts, reducing maintenance and increasing operational efficiency.
A key component in the system is the pressure vessel or bin, which maintains a slight overpressure to keep the material in a fluidized state. This fluidization ensures that the material can be easily and uniformly discharged when the valve is opened. The air flow is carefully regulated to match the material's characteristics, such as density and particle size, to achieve optimal conveying performance. The metering function is achieved by controlling the duration of the valve opening, allowing precise control over the amount of material transported per cycle. This precision is critical in applications where accurate dosing is required, such as in chemical processing or pharmaceutical manufacturing.
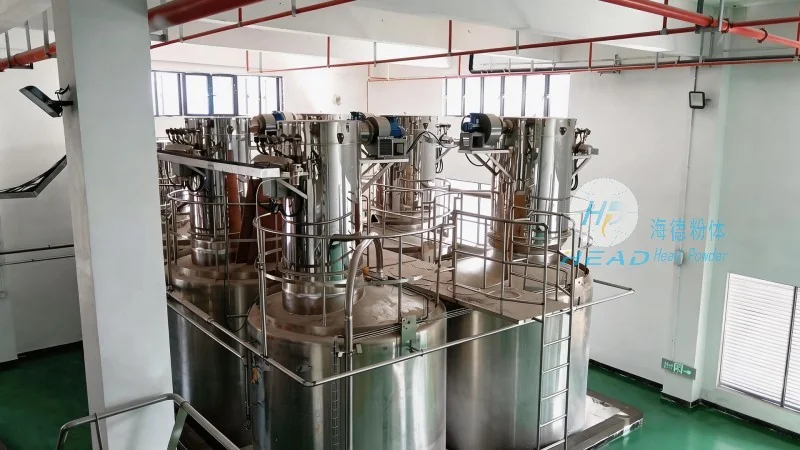
Key Features of Metering Bin Pump Pneumatic Conveying Equipment
One of the primary advantages of metering bin pumps is their ability to handle a wide range of materials, including abrasive, corrosive, or temperature-sensitive substances. The absence of moving parts in the conveying line minimizes wear and tear, extending the equipment's service life. Additionally, the system is highly flexible, allowing for easy integration with existing infrastructure and adaptation to different process requirements. The metering capability ensures consistent material flow, reducing variations in downstream processes and improving overall product quality.
Another notable feature is the self-cleaning design, which prevents material buildup and clogging in the pipeline. The pressurized air helps to maintain a clean system by continuously flushing the lines, ensuring that no residue remains after material transport. This feature is particularly beneficial for handling sticky or cohesive materials that are prone to blockages in traditional conveying systems. The equipment also offers high efficiency in terms of energy consumption, as the compressed air is used efficiently to move the material without excessive waste. This makes it an environmentally friendly option compared to other bulk material handling methods.
Applications and Benefits in Industrial Settings
Metering bin pumps are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, they are employed to transport ingredients like flour, sugar, and spices, ensuring hygienic and contamination-free handling. In pharmaceutical manufacturing, the precise dosing and clean design of the equipment meet stringent regulatory requirements for product safety and quality. The chemical industry benefits from the ability to handle corrosive materials without damaging the equipment, while the mining sector uses it to transport minerals and ores from storage bins to processing plants.
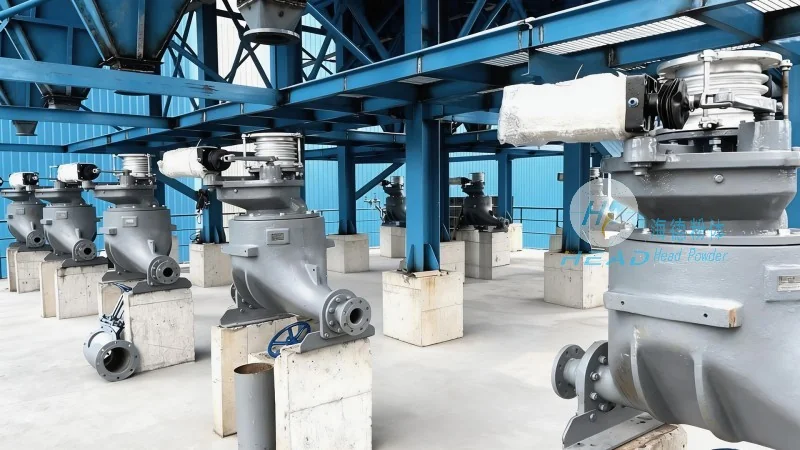
The benefits of using metering bin pumps extend beyond operational efficiency. The reduced maintenance requirements lower long-term costs, and the consistent material flow improves production throughput. The flexibility of the system allows for easy adjustments to production rates, making it suitable for both continuous and batch operations. Furthermore, the equipment's compact design saves space in industrial facilities, which is particularly valuable in urban or space-constrained environments.
Conclusion and Company Information
Understanding the working principle and features of metering bin pump pneumatic conveying equipment is essential for optimizing material handling processes in industrial settings. The combination of precise metering, efficient air utilization, and robust design makes this equipment a reliable choice for a wide range of applications. For companies seeking high-quality and reliable pneumatic conveying solutions, Shandong HeadPowder Engineering Co., Ltd. offers expertly engineered products tailored to specific operational needs. With a focus on innovation and customer satisfaction, HeadPowder provides comprehensive support from design to installation, ensuring that clients achieve optimal performance and cost-effectiveness in their material handling operations.