

Operation Process and Working Principle of Coal and Stone Powder Pneumatic Conveying Equipment
Pneumatic conveying equipment, particularly for coal and stone powders, plays a crucial role in modern industrial operations. As a specialized solution for handling bulk materials, this equipment ensures efficient, safe, and reliable transportation of fine powders and granular materials. HeadPowder, a leading manufacturer based in Shandong, China, specializes in designing and producing high-quality pneumatic conveying systems tailored to meet diverse industrial needs. This article provides an in-depth look at the operation process and working principle of such equipment, highlighting its technical aspects and practical applications.
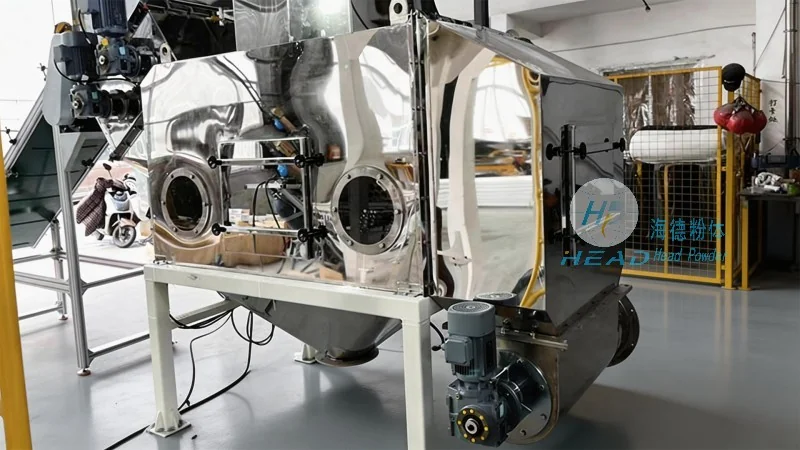
Working Principle of Pneumatic Conveying Systems
The core principle of pneumatic conveying involves using compressed air or gas to transport solid materials through a pipeline. In the case of coal and stone powders, the system typically operates under positive pressure, where air is forced through the pipeline to move the material. The process relies on the interaction between the air flow and the material particles, creating a suspension that allows for smooth movement. Key components include a blower or compressor, a hopper for material storage, a conveying line, and a discharge point. The blower generates the necessary pressure to propel the material, while the hopper ensures a consistent feed. The conveying line may include bends, expansions, or filters to maintain material flow and prevent blockages. This principle enables the equipment to handle materials that are difficult to transport via traditional methods, such as those with high moisture content or abrasive properties.
Operation Process of Coal and Stone Powder Conveying Equipment
The operation process of coal and stone powder pneumatic conveying equipment follows a systematic sequence to ensure optimal performance. The process begins with the preparation phase, where the material is loaded into the hopper. The hopper is equipped with a feeder, such as a rotary valve or a screw feeder, which controls the flow rate of the material into the conveying line. Once the system is ready, the blower is activated, generating the required air pressure. As the air flows through the pipeline, it picks up the material from the hopper, forming a dense phase or dilute phase suspension depending on the system design. The material is then transported to the discharge point, where it is released into a storage bin or processing unit. The system operates continuously, with the feeder adjusting the material flow to match the air flow rate. During operation, operators monitor key parameters such as air pressure, material flow rate, and system pressure drop to ensure smooth operation. If any issues arise, such as blockages or pressure drops, the system may trigger alarms or automatic shut-downs to prevent damage. The entire process is designed to be efficient, with minimal downtime and high material throughput, making it ideal for industrial applications where consistent material supply is critical.
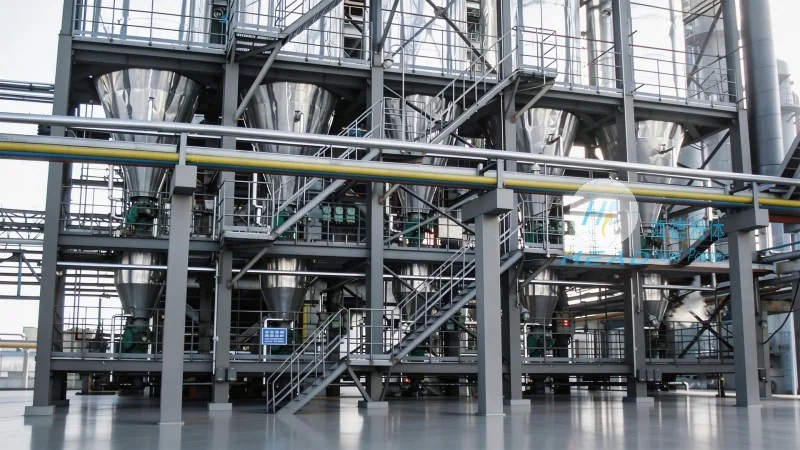
Technical Features and Advantages of the Equipment
Coal and stone powder pneumatic conveying equipment from HeadPowder offers several technical features and advantages that enhance its performance and reliability. One key feature is the use of positive pressure systems, which are effective for transporting fine powders and preventing material degradation. The equipment is designed with robust materials, such as stainless steel or corrosion-resistant alloys, to withstand the abrasive nature of coal and stone powders. This ensures long service life and minimal maintenance. Another advantage is the flexibility in system design, allowing customization to suit specific industrial requirements. For example, the conveying line can be adjusted in length and diameter to accommodate different material quantities and distances. The system also includes advanced control systems, such as PLC (Programmable Logic Controller) integration, which allows for automated operation and real-time monitoring. This enhances operational efficiency and reduces the need for manual intervention. Additionally, the equipment is designed with safety features, including pressure relief valves and emergency shut-off mechanisms, to protect operators and the system from potential hazards. These features collectively make the equipment a reliable and efficient solution for handling coal and stone powders in various industrial settings.
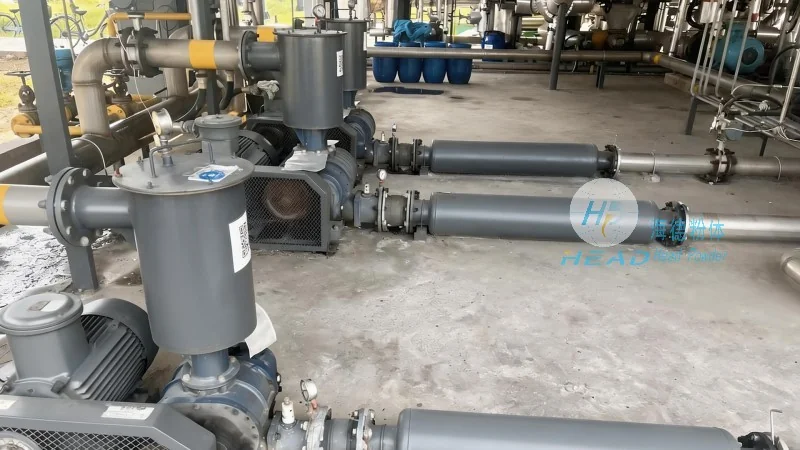
Application Scenarios and Industrial Use Cases
The coal and stone powder pneumatic conveying equipment is widely used in various industrial sectors, including power generation, mining, and chemical processing. In power plants, it is used to transport coal from storage silos to boilers, ensuring a continuous supply of fuel. The equipment is also employed in mining operations to transport crushed stone and ore from processing plants to storage facilities. In the chemical industry, it handles fine powders such as limestone, clay, and other raw materials, facilitating their transport to production lines. The versatility of the system allows it to handle different material types, including those with varying particle sizes and moisture content. For example, in a cement plant, the equipment transports raw materials like limestone and clay to the grinding mills, where they are processed into cement. The consistent and efficient material transport provided by the system improves overall production efficiency and reduces operational costs. Additionally, the equipment is suitable for applications where dust control is critical, as the enclosed system minimizes dust emissions and improves workplace safety. These applications highlight the importance of the equipment in modern industrial operations, where reliable material handling is essential for maintaining productivity and meeting operational demands.
Conclusion and Company Overview
Coal and stone powder pneumatic conveying equipment is a vital component in modern industrial processes, offering efficient and reliable transportation of bulk materials. The operation process, which involves material loading, air compression, and continuous transport, ensures high throughput and minimal downtime. The working principle, based on positive pressure and air suspension, enables the equipment to handle difficult-to-transport materials effectively. HeadPowder, with its expertise in designing and manufacturing such equipment, provides high-quality solutions tailored to specific industrial needs. Based in Shandong, China, the company leverages advanced technology and robust design to deliver equipment that meets the demands of various industries. The technical features and advantages of the equipment, including durability, flexibility, and safety, make it a preferred choice for industrial applications. As industrial operations continue to evolve, the importance of efficient material handling will only increase, and pneumatic conveying equipment will remain a key solution. HeadPowder's commitment to quality and innovation ensures that its products continue to meet the changing needs of the industry, providing reliable and efficient solutions for coal and stone powder transportation.