

Operation Process and Working Principle of Tonne Bag Powder Pneumatic Conveying System
HeadPowder, a leading provider in the field of bulk material handling, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. This article provides a detailed overview of the operation process and working principle of tonne bag powder pneumatic conveying systems, highlighting the key components, operational steps, and technical aspects that ensure efficient and reliable material transport.
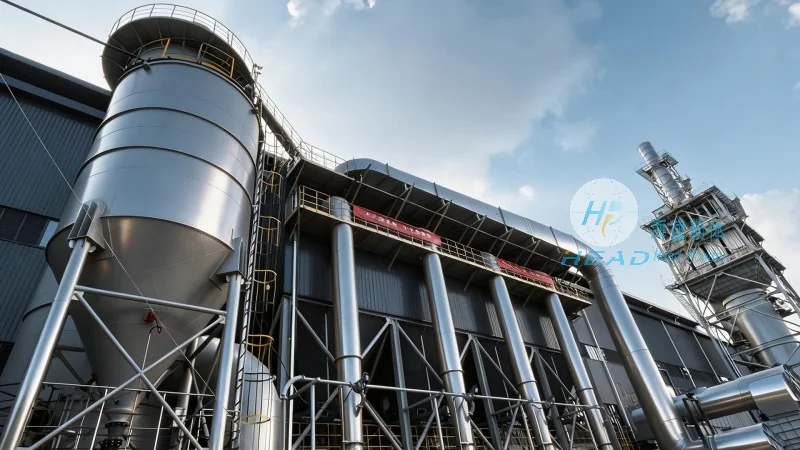
Understanding Tonne Bag Powder Pneumatic Conveying Systems
A tonne bag powder pneumatic conveying system is a sophisticated piece of equipment used to transport bulk powders from a storage container, typically a tonne bag, to a processing or storage location. The system operates on the principle of pneumatic transport, utilizing air pressure to move the material through a pipeline network. This method offers several advantages over traditional mechanical conveying systems, including reduced maintenance, lower energy consumption, and the ability to handle materials that are difficult to transport using other methods.
Key Components of the System
The tonne bag powder pneumatic conveying system consists of several critical components that work in tandem to achieve efficient material transport. These components include:
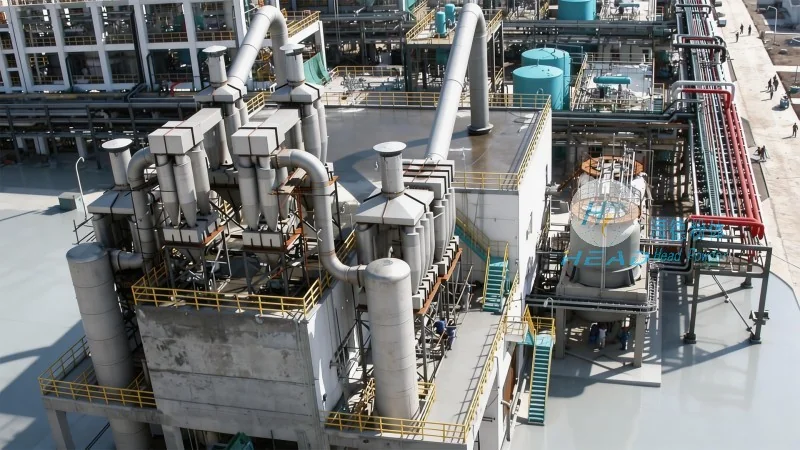
- Tonne Bag Discharge Unit: This component is responsible for opening the tonne bag and releasing the powder into the system. It typically includes a hopper, a valve mechanism, and a feeding device that ensures a consistent flow of material.
- Pneumatic Conveying Pipeline: The pipeline is the main pathway for transporting the powder. It is usually made of stainless steel or other corrosion-resistant materials to handle various types of powders and prevent contamination.
- Air Supply System: This system provides the necessary air pressure and volume to move the powder through the pipeline. It includes a blower or compressor, air filters, and pressure regulators to maintain optimal operating conditions.
- Control System: The control system monitors and regulates the operation of the entire system, ensuring that the flow rate, pressure, and other parameters are maintained within safe and efficient limits.
- Receiving Hopper or Storage Tank: The final component where the powder is deposited after being conveyed through the pipeline.
Operation Process of the System
The operation of a tonne bag powder pneumatic conveying system involves several sequential steps, each designed to ensure smooth and continuous material transport. The process typically begins with the preparation of the tonne bag and the system setup. Here are the key operational steps:
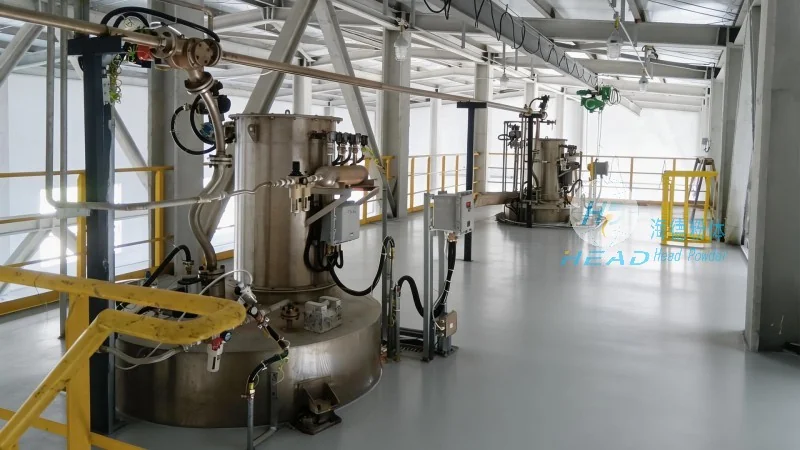
- System Preparation: The tonne bag is placed in the discharge unit, and the system is checked for proper operation, including air pressure, valve positions, and pipeline integrity.
- Opening the Tonne Bag: The discharge unit opens the tonne bag, allowing the powder to fall into the hopper. This step may involve mechanical or pneumatic assistance to ensure complete discharge.
- Material Feeding: The powder is fed from the hopper into the pneumatic conveying pipeline. The feeding rate is controlled by the control system to maintain a consistent flow.
- Pneumatic Conveying: The air supply system generates the necessary pressure, and the powder is carried through the pipeline by the air flow. The air-powder mixture travels at high velocity, ensuring efficient transport.
- Receiving and Storage: The powder is deposited into the receiving hopper or storage tank. The control system monitors the level of the receiving container and adjusts the feeding rate as needed.
- System Shutdown: Once the tonne bag is empty, the system is shut down in an orderly manner, including closing the valves, releasing pressure, and cleaning the system if necessary.
Working Principle of the System
The working principle of a tonne bag powder pneumatic conveying system is based on the fundamental physics of fluid dynamics and particle transport. The system operates by creating a pressure differential between the inlet and outlet of the pipeline. The blower or compressor provides the motive force, generating a high-pressure air stream that entrains the powder particles and moves them through the pipeline. The air-powder mixture is then separated at the receiving end, typically using a cyclone or other separation device, and the air is either recirculated or vented to the atmosphere.
Advantages of Tonne Bag Powder Pneumatic Conveying Systems
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of tonne bag powder pneumatic conveying systems. With a focus on innovation and quality, the company offers customized solutions that meet the specific needs of various industries. The operation process and working principle of these systems ensure efficient and reliable material transport, making them an ideal choice for bulk powder handling applications. By understanding the key components and operational steps, users can optimize the performance of the system and maximize its benefits.