

[Pneumatic Conveying Technology for Powdered Fermentation Agents: Principles, Applications, and Development Trends]
HeadPowder, a leading provider in the field, specializes in advanced solutions for the efficient handling of powdered fermentation agents. This article explores the fundamental principles, practical applications, and emerging trends in pneumatic conveying technology, offering insights into how these systems enhance operational efficiency and product quality in industrial settings.
Principles of Pneumatic Conveying for Powdered Fermentation Agents
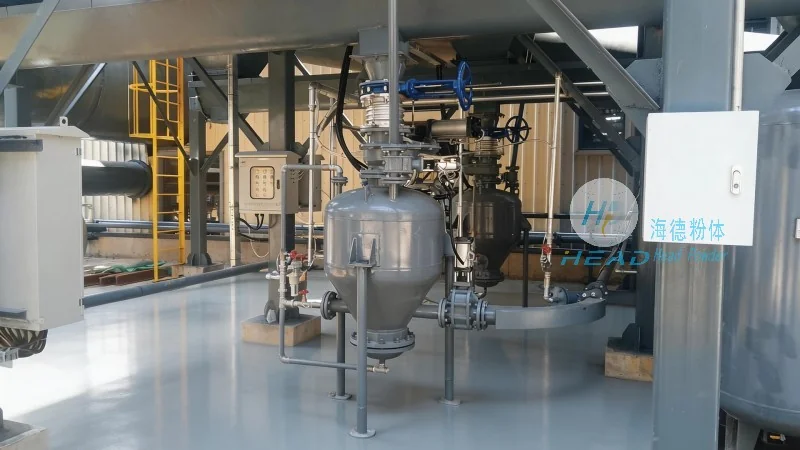
Pneumatic conveying systems utilize air or gas to transport bulk materials, such as powdered fermentation agents, through a network of pipes. The core principle involves creating a pressure differential that propels the material from the source to the destination. There are two primary types of pneumatic conveying: dilute-phase and dense-phase. Dilute-phase systems operate at low pressure, using high-velocity air to suspend particles, while dense-phase systems employ higher pressure and lower velocity to move material in a more controlled manner. The choice between these systems depends on factors like material properties, distance, and required flow rates. For powdered fermentation agents, which often have fine particle sizes and varying moisture content, the selection of an appropriate conveying method is critical to prevent agglomeration and maintain product integrity.
Applications of Pneumatic Conveying in Fermentation Agent Processing
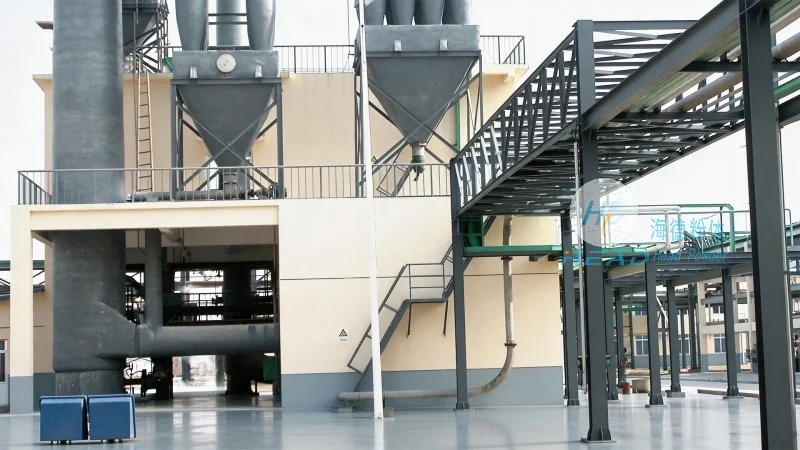
HeadPowder's pneumatic conveying solutions are widely applied in the processing of powdered fermentation agents across various industries. In the food and beverage sector, these systems are used to transport ingredients like yeast, enzymes, and flavor enhancers from storage silos to production lines, ensuring a continuous and hygienic flow. The pharmaceutical industry also benefits from this technology, as it allows for the safe and sterile transfer of active fermentation components, minimizing contamination risks. Additionally, in the chemical and biotechnology fields, pneumatic conveying is employed to move raw materials and finished products, supporting processes like fermentation, drying, and packaging. The versatility of these systems makes them suitable for both small-scale laboratory applications and large-scale industrial operations, adapting to the specific needs of each facility.
Advancements and Future Trends in Pneumatic Conveying Technology
The field of pneumatic conveying for powdered fermentation agents is continuously evolving, driven by technological advancements and increasing demand for efficiency. Modern systems now incorporate advanced control systems, allowing for real-time monitoring and adjustment of air pressure, flow rates, and material transport. This integration enhances process control and reduces downtime. Additionally, the development of more energy-efficient pumps and compressors has led to reduced operational costs and lower environmental impact. Emerging trends include the use of smart sensors to detect material blockages or changes in flow, enabling proactive maintenance and preventing system failures. Furthermore, the integration of automation and robotics in conveying systems is improving safety and productivity, particularly in environments where human exposure to powders is minimized. As the industry moves toward more sustainable and high-performance solutions, the future of pneumatic conveying for fermentation agents looks promising, with ongoing innovations aimed at optimizing material handling and enhancing overall operational performance.
Conclusion and Company Overview
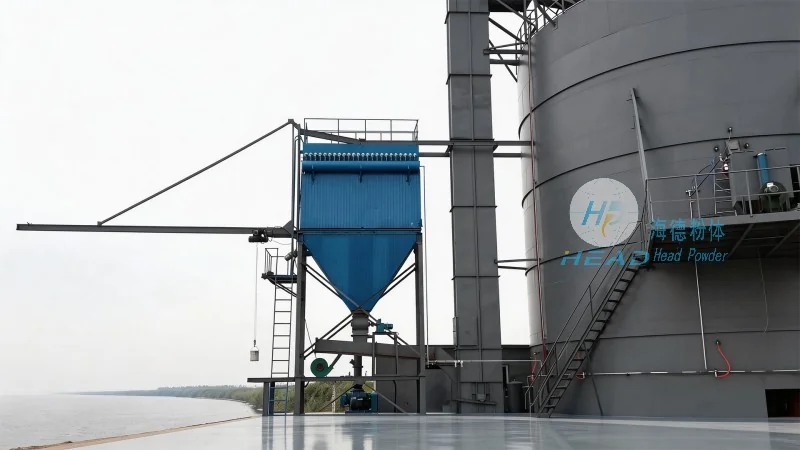
HeadPowder Engineering Co., Ltd., based in Shandong, China, remains at the forefront of pneumatic conveying technology for powdered fermentation agents. With a commitment to innovation and customer satisfaction, the company provides tailored solutions that address the unique challenges of each application. By leveraging advanced engineering and continuous research, HeadPowder ensures that its systems meet the highest standards of efficiency, reliability, and safety. As the demand for efficient material handling in the fermentation industry grows, the company's expertise and cutting-edge technology position it as a key partner for businesses seeking to optimize their processes and enhance product quality. The future of pneumatic conveying, as applied to powdered fermentation agents, is bright, with HeadPowder poised to lead the way in delivering advanced solutions that drive industry progress.