

What is an Intelligent Bulk Material Pneumatic Conveying Equipment? What are its Design Principles?
Intelligent bulk material pneumatic conveying equipment represents a sophisticated solution in material handling technology, designed to efficiently transport bulk materials from one location to another with precision and reliability. This equipment is widely used in various industries, including food processing, pharmaceuticals, chemicals, and more, where the handling of powders and granules requires strict control over flow, purity, and safety.
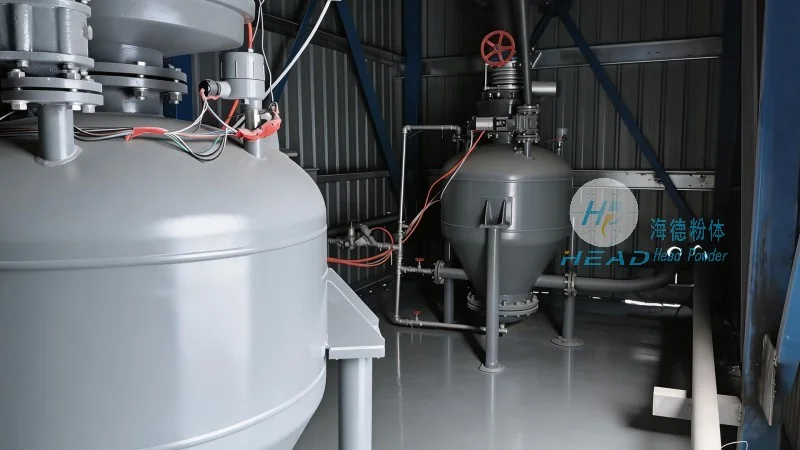
Design Principles of Intelligent Bulk Material Pneumatic Conveying Equipment
The core design principle of such equipment revolves around the use of compressed air to create a flow of material through a pipeline system. This pneumatic conveying method is based on the fundamental physics of fluid dynamics, where the material is suspended and transported by the air stream. The intelligent aspect of these systems is enhanced through advanced control technologies, including sensors, automation, and data processing, which enable real-time monitoring and adjustment of the conveying process. This integration of traditional pneumatic conveying with modern intelligent control systems ensures optimal performance, reduced downtime, and improved operational efficiency.
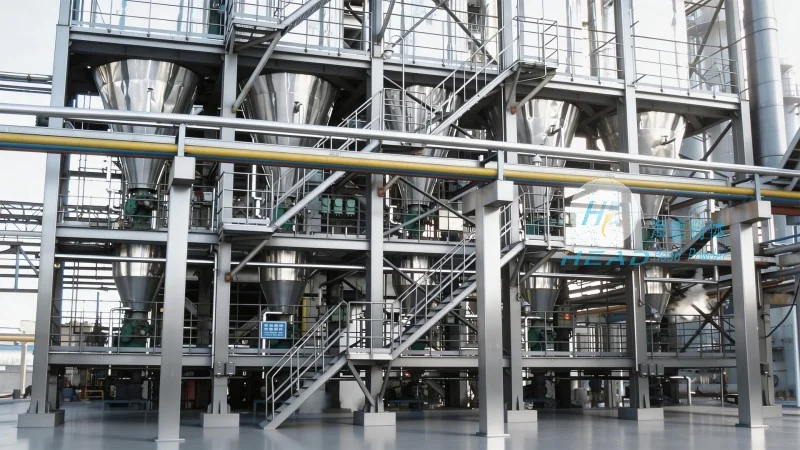
Key Components and Their Functions
The intelligent bulk material pneumatic conveying equipment typically consists of several key components, each playing a crucial role in the overall operation. These components include the material feed hopper, which holds the bulk material and controls the feed rate; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying pipeline, which transports the material from the feed point to the discharge point; and the control system, which manages the entire process. Additionally, features like dust collection systems, material separation units, and safety interlocks are often integrated to enhance operational safety and material quality.
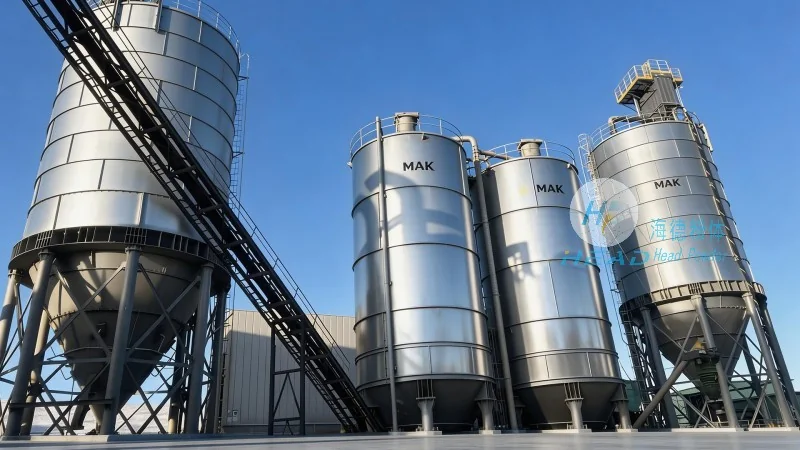
Advantages of Using Intelligent Pneumatic Conveying Systems
Implementing intelligent bulk material pneumatic conveying equipment offers numerous advantages over traditional methods. Firstly, it provides a highly efficient and continuous material transport solution, reducing the need for manual handling and minimizing the risk of material contamination. The precise control capabilities allow for accurate dosing and mixing of materials, which is critical in industries like pharmaceuticals and food processing where product consistency is paramount. Furthermore, the intelligent control systems enable energy optimization by adjusting air pressure and flow rates based on real-time conditions, leading to cost savings and reduced environmental impact. Safety is another significant benefit, as the integrated safety features prevent accidental releases and ensure compliance with industry regulations.
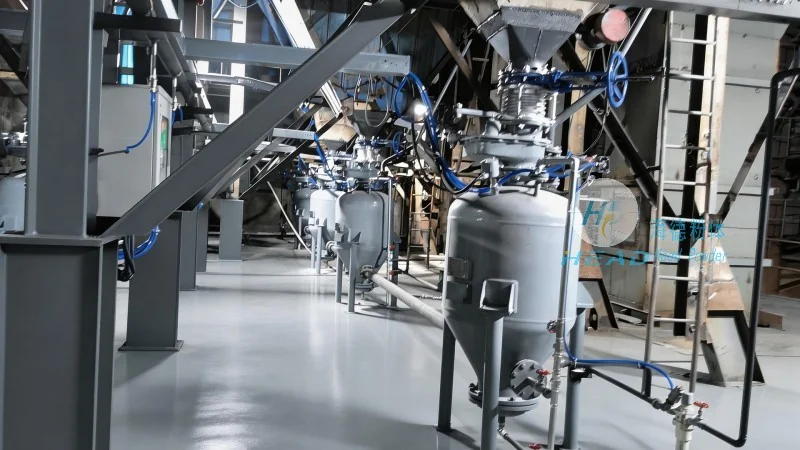
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design, development, and production of advanced material handling equipment. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of clients. The company is headquartered in Shandong, China, and leverages its expertise in engineering and technology to deliver reliable and efficient equipment that meets the highest standards of performance and safety. HeadPowder's commitment to customer satisfaction and technological advancement ensures that its products remain at the forefront of material handling solutions.