

Working Principle and Features of Compound Fertilizer Pneumatic Conveying System Equipment
Compound fertilizer pneumatic conveying systems are critical in modern fertilizer processing and distribution, offering efficient and reliable methods for transporting bulk materials. This article explores the working principles and key features of such systems, providing insights into their functionality and advantages.
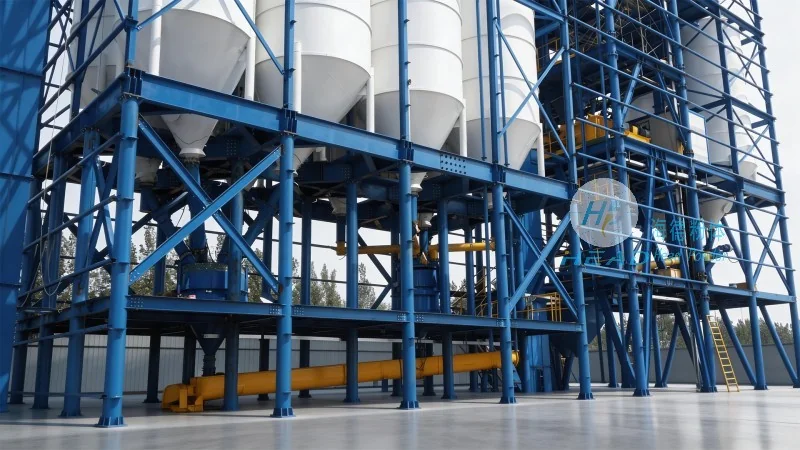
Understanding the Working Principle of Pneumatic Conveying Systems
The core of a compound fertilizer pneumatic conveying system lies in its ability to transport bulk materials using air pressure. These systems typically operate through two main mechanisms: positive pressure and negative pressure (or vacuum) conveying. In positive pressure systems, a fan or blower generates high-pressure air that propels the material through a pipeline. The material is often fed into the system via a hopper or feeder, where it is mixed with the air stream. As the air flows through the pipeline, it carries the fertilizer particles to the destination point, such as a storage silo or processing unit. The system then separates the material from the air using a cyclone separator or other filtration equipment, allowing the air to be recycled or released.
Negative pressure systems, on the other hand, create a vacuum in the pipeline, drawing the material from the source into the system. The material is fed into the pipeline, and the vacuum pulls it along with the air stream. This method is particularly useful for applications where dust control is a priority, as the system operates under negative pressure, preventing dust from escaping into the environment. Both positive and negative pressure systems can be customized to handle different types of compound fertilizers, including granular, powdered, or mixed formulations, ensuring versatility in material handling.
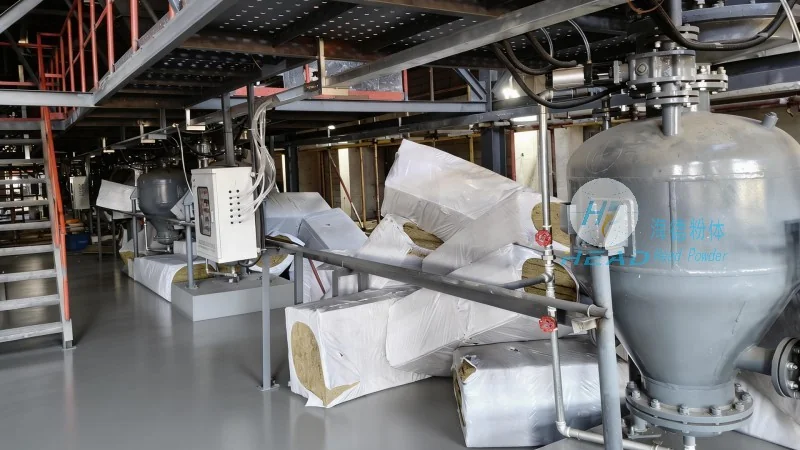
Key Features and Advantages of Compound Fertilizer Pneumatic Conveying Systems
One of the primary advantages of pneumatic conveying systems is their high efficiency in material transport. Unlike traditional methods like belt conveyors or bucket elevators, pneumatic systems can handle large volumes of material with minimal labor and space requirements. This makes them ideal for industrial-scale fertilizer production and distribution, where speed and throughput are critical. Additionally, these systems offer excellent dust control, as the material is contained within the pipeline, reducing the risk of dust exposure for workers and minimizing environmental impact.
Another significant feature is the flexibility of pneumatic conveying systems. They can be easily integrated into existing production lines or expanded to accommodate increased production capacity. The modular design allows for customization based on specific application needs, such as varying material types, processing speeds, or destination locations. This adaptability makes them a cost-effective solution for fertilizer manufacturers looking to optimize their operations.
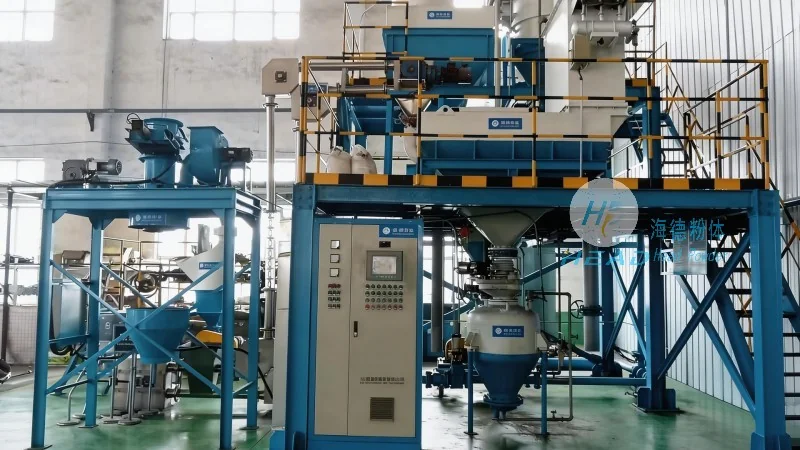
Furthermore, pneumatic conveying systems contribute to improved safety and operational reliability. By eliminating the need for manual handling of bulk materials, these systems reduce the risk of accidents and injuries. The enclosed pipeline design also minimizes the risk of material spillage or contamination, ensuring product quality and consistency. In terms of maintenance, modern pneumatic systems are equipped with advanced monitoring and control technologies, allowing for real-time performance tracking and predictive maintenance, which further enhances operational efficiency.
Applications and Industries Served by Pneumatic Conveying Systems
Compound fertilizer pneumatic conveying systems are widely used in various industries, including agricultural, industrial, and chemical sectors. In the agricultural industry, these systems are essential for transporting fertilizers from production facilities to farms or storage depots, ensuring timely delivery and efficient distribution. In industrial applications, they are used in fertilizer manufacturing plants to move raw materials, intermediate products, and finished goods between processing stages. The chemical industry also benefits from these systems, as they can handle a variety of chemical powders and granules, including those with high moisture content or abrasive properties.
The versatility of pneumatic conveying systems makes them suitable for a range of applications, from small-scale farm operations to large-scale industrial plants. Whether used for transporting granular urea, powdered ammonium nitrate, or mixed NPK fertilizers, these systems provide reliable and efficient material handling solutions. The ability to handle different material characteristics, such as particle size, density, and moisture content, makes them a preferred choice for many fertilizer producers.
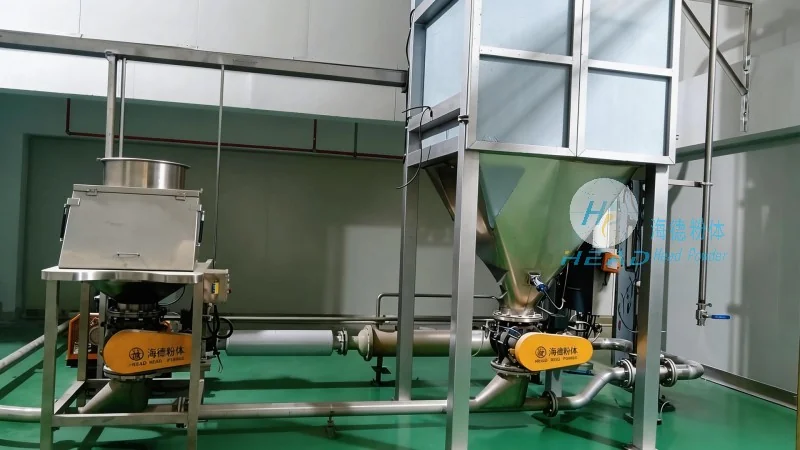
Conclusion: The Role of Pneumatic Conveying Systems in Modern Fertilizer Handling
In conclusion, compound fertilizer pneumatic conveying systems represent a sophisticated and efficient solution for bulk material transport in the fertilizer industry. Their working principles, based on air pressure and vacuum, enable high-speed, dust-free, and flexible material handling. The key features, including high efficiency, excellent dust control, and operational reliability, make these systems indispensable in modern fertilizer processing and distribution. As the demand for efficient and sustainable fertilizer handling solutions continues to grow, pneumatic conveying systems remain a vital component in meeting industry needs.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field, specializes in designing and supplying customized pneumatic conveying systems tailored to the specific requirements of fertilizer manufacturers. With years of experience and a commitment to quality, HeadPowder provides reliable equipment that enhances operational efficiency and ensures product safety. The company's expertise in material handling technology, combined with its focus on customer needs, makes it a trusted partner for businesses seeking to optimize their fertilizer processing and distribution operations.