

Operation Process and Working Principle of Camellia Seed Material Handling System Equipment
Camellia seed material handling systems are critical components in the oil extraction industry, particularly for businesses involved in processing camellia seeds to extract oil. These systems are engineered to efficiently transport raw camellia seeds through various stages of processing, from initial collection and cleaning to storage and subsequent processing steps like crushing or pressing. The seamless operation of these systems directly impacts the overall productivity, efficiency, and quality of the entire oil production process.
Company Introduction
HeadPowder, a prominent manufacturer in the field, specializes in the design, development, and production of advanced material handling equipment. As Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, the company has established a strong reputation for delivering high-quality, reliable systems tailored to the specific needs of the oil processing sector. With a focus on innovation and customer-centric solutions, HeadPowder ensures its equipment meets the rigorous demands of modern industrial applications, providing durability and performance.
Overview of the Material Handling System
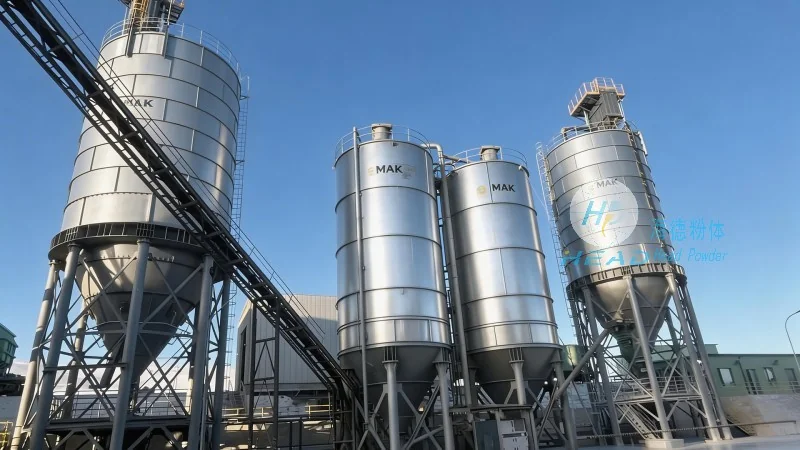
The camellia seed material handling system typically comprises interconnected components such as feeders, conveyors, elevators, and storage bins. Each component plays a vital role in the smooth movement of seeds through the processing line. The system is designed to accommodate the unique characteristics of camellia seeds, including their size, density, and moisture content, ensuring minimal loss and maximizing throughput. This integrated approach minimizes bottlenecks and enhances operational efficiency.
Operation Process
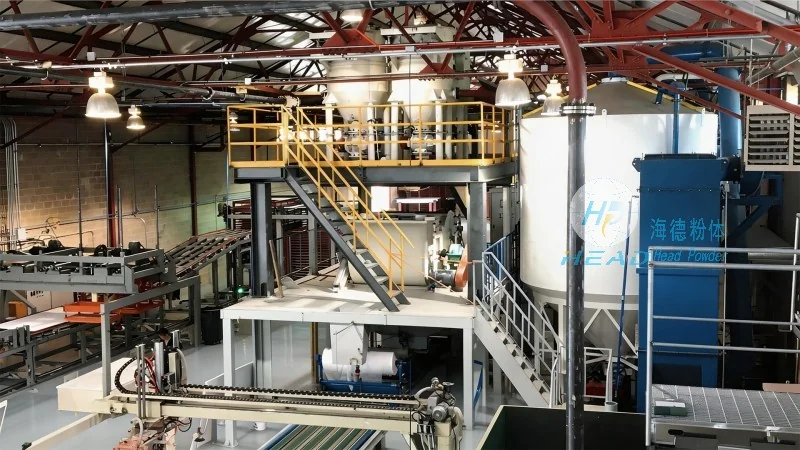
The operation of the camellia seed material handling system begins with the intake of raw seeds. Seeds are first stored in a hopper or storage bin, where they are held until processing begins. A feeder mechanism, often rotary or vibratory, regulates the flow of seeds into the primary conveyor system. The conveyor—whether a belt, screw, or pneumatic type—transports seeds to the next processing stage. At each stage, cleaning mechanisms remove impurities like dust, debris, or foreign materials. The seeds then proceed to crushing or pressing equipment, where oil extraction continues.
Working Principle
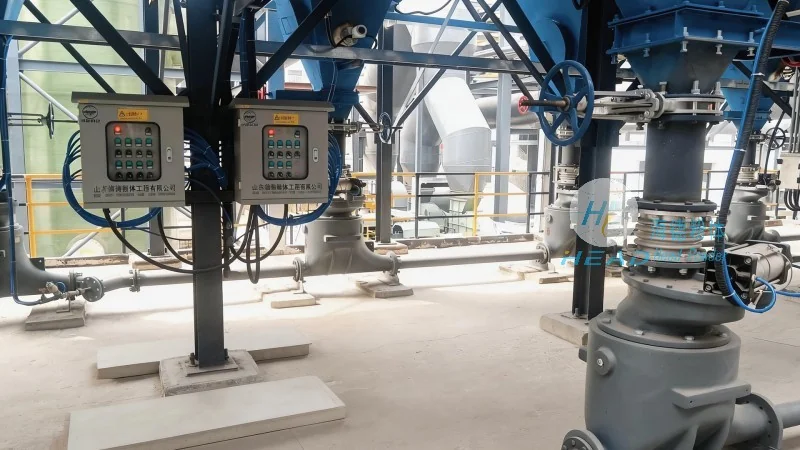
The working principle of the material handling system relies on mechanical and sometimes pneumatic forces to move seeds through the processing line. The feeder ensures a consistent, controlled flow, preventing overloading or underloading of the conveyor. The conveyor system uses friction or air pressure to move seeds along the path. Elevators lift seeds to higher levels for storage or upper processing units. A centralized control panel monitors flow rate, pressure, and other critical parameters, enabling real-time adjustments for optimal operation. This control system enhances efficiency and safety.
Key Features and Benefits
HeadPowder's camellia seed material handling systems incorporate advanced features that enhance performance and reliability. Adjustable speed controls for feeders and conveyors allow operators to match flow rates to processing capacity. Durable materials like stainless steel withstand the abrasive nature of seeds and harsh processing conditions. The design minimizes material loss and contamination, ensuring high-quality output. These features lead to improved productivity, reduced maintenance costs, and enhanced operational safety.
Application in Oil Processing
In oil processing, the material handling system maintains a continuous flow of raw materials, reducing downtime and increasing oil yield. By efficiently transporting seeds from storage to extraction equipment, the system supports cost savings and operational efficiency. Its design allows easy integration with other processing equipment (e.g., crushers, presses), creating a seamless production line. This integration optimizes workflow and ensures consistent output quality.
Conclusion
Camellia seed material handling systems, exemplified by those from HeadPowder, are essential for efficient oil processing operations. The combination of advanced technology, robust engineering, and meticulous design ensures these systems can handle the unique challenges of camellia seed processing. Understanding the operation process and working principle of such systems enables manufacturers and operators to optimize production lines, improve productivity, and achieve better economic outcomes. HeadPowder's commitment to quality and innovation continues to set industry standards, providing reliable solutions for the oil processing sector.