

Operation Process and Working Principle of Intelligent Powder Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced powder handling equipment. Among their innovative offerings is the intelligent powder pneumatic conveying system, which integrates cutting-edge technology to enhance efficiency and reliability in material transport. This article delves into the operation process and working principles of this sophisticated equipment, providing a comprehensive understanding of its functionality and benefits.
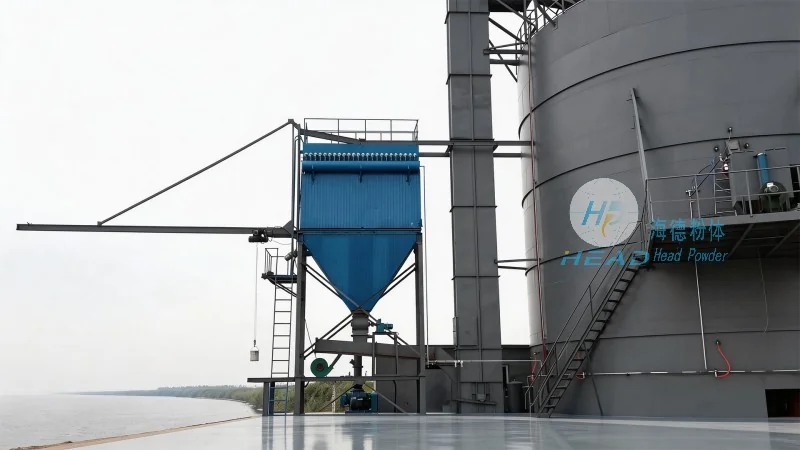
Overview of Intelligent Powder Pneumatic Conveying Systems
The intelligent powder pneumatic conveying machine is engineered to transport bulk powders and granular materials over short to medium distances using air as the conveying medium. Unlike traditional mechanical systems, this technology offers a dust-free, low-maintenance solution that is ideal for industries such as pharmaceuticals, food processing, and chemical manufacturing. The system combines precision control, real-time monitoring, and automated operations to ensure optimal performance and safety.
Key Components and Their Functions
The intelligent powder pneumatic conveying system consists of several critical components, each playing a vital role in the overall operation. These include the hopper for material storage, the air compressor or blower to generate the conveying air, the pipeline network for material transport, the control system for process management, and the discharge unit for material release. Each component is designed with durability and efficiency in mind, ensuring seamless integration and reliable performance.
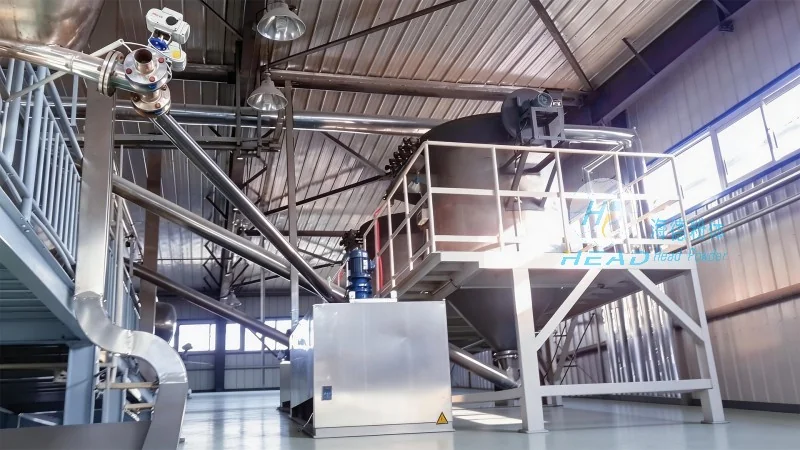
Operation Process: Step-by-Step Breakdown
The operation of the intelligent powder pneumatic conveying machine follows a systematic process that ensures consistent and controlled material transport. The process begins with the loading of the hopper, where bulk powders are introduced into the system. The control system then activates the air compressor, which generates a flow of air at a specific pressure and volume. This air is directed through the pipeline network, creating a pressure differential that draws the powder particles into the conveying stream. As the material travels through the pipes, it is suspended and transported to the discharge point. The control system continuously monitors parameters such as air pressure, flow rate, and material level, adjusting operations as needed to maintain optimal conditions. Once the material reaches the discharge unit, it is released into the target container or processing equipment. The system then returns to standby mode, ready for the next cycle.
Working Principles: How It Works
The working principle of the intelligent powder pneumatic conveying system is based on the fundamental concept of pneumatic transport, where air is used to move solid particles. The system operates under either positive or negative pressure, depending on the application requirements. In positive pressure systems, the air compressor pushes air through the pipeline, creating a pressure higher than the ambient air, which propels the powder forward. In negative pressure systems, the blower creates a vacuum, drawing air and material into the pipeline. The intelligent features of the system enhance this process by incorporating sensors and automation, allowing for real-time adjustments and predictive maintenance. This ensures that the conveying process is efficient, safe, and adaptable to varying material characteristics and operational conditions.
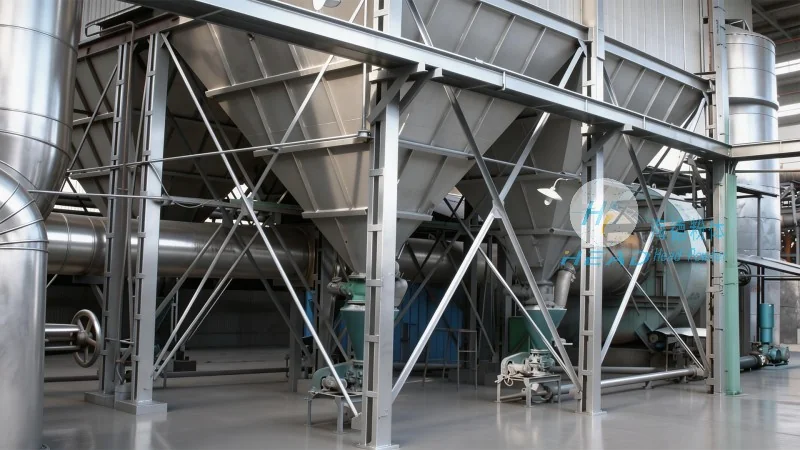
Advantages and Applications
The intelligent powder pneumatic conveying machine offers numerous advantages over traditional transport methods. These include reduced dust generation, improved material handling safety, lower maintenance costs, and enhanced process control. The system is particularly suitable for transporting sensitive materials that require a clean and hygienic environment, such as pharmaceutical powders or food ingredients. Additionally, its modular design allows for customization to meet specific application needs, making it a versatile solution for various industries. HeadPowder's commitment to innovation ensures that their systems are equipped with the latest technology to deliver superior performance and reliability.
Conclusion
In conclusion, the intelligent powder pneumatic conveying machine represents a significant advancement in powder handling technology. By integrating advanced control systems and automation, this equipment provides an efficient, reliable, and safe solution for transporting bulk materials. HeadPowder's expertise in engineering and manufacturing ensures that their systems meet the highest standards of performance and durability. For industries seeking to optimize their material transport processes, the intelligent powder pneumatic conveying machine is an excellent choice that combines functionality with cutting-edge technology.