

Operation Process and Working Principle of Intelligent Tonne Bag Feeding Station Material Pneumatic
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in the design, production, and installation of material handling equipment. The company is headquartered in Shandong, China, and has established a strong reputation in the industry for its innovative solutions and reliable products. Among its product portfolio is the intelligent tonne bag feeding station with material pneumatic conveying line, a system engineered to enhance material handling efficiency and precision in various industrial applications.
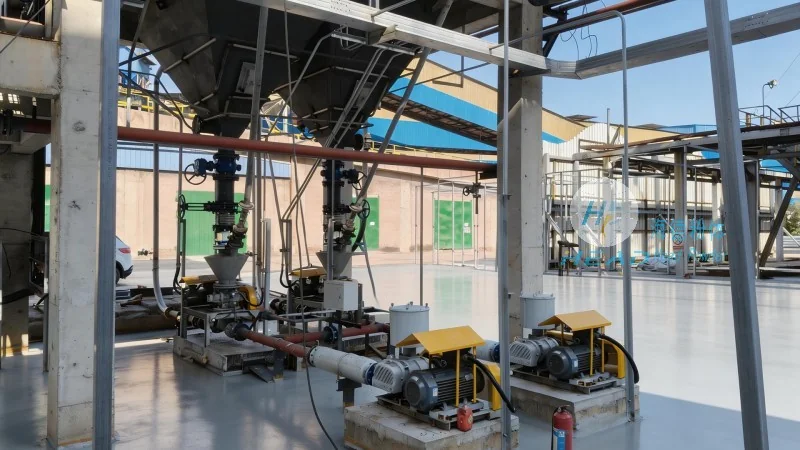
Overview of the Intelligent Tonne Bag Feeding Station Material Pneumatic Conveying Line
The intelligent tonne bag feeding station material pneumatic conveying line is a comprehensive system designed to automate the process of receiving, opening, and transferring bulk materials from tonne bags into processing equipment. This system integrates advanced automation technologies and robust pneumatic conveying mechanisms to ensure smooth, safe, and efficient material flow. The key components include the tonne bag handling unit, material opening and feeding mechanism, pneumatic conveying pipeline system, and control system, all working in harmony to achieve seamless operation.
Key Components and Their Functions
The system comprises several critical components, each playing a vital role in the overall operation. The tonne bag handling unit is responsible for receiving and positioning the tonne bags, typically using a mechanical lifting or conveyor system. The material opening mechanism, often equipped with a hydraulic or pneumatic cutter, safely opens the bag without damaging the contents. The feeding mechanism then transfers the material from the bag into the conveying pipeline. The pneumatic conveying pipeline system, which may include a combination of positive and negative pressure conveying methods, transports the material to the target processing location. The control system, equipped with sensors and programmable logic controllers (PLCs), monitors and regulates the entire process to ensure optimal performance and safety.
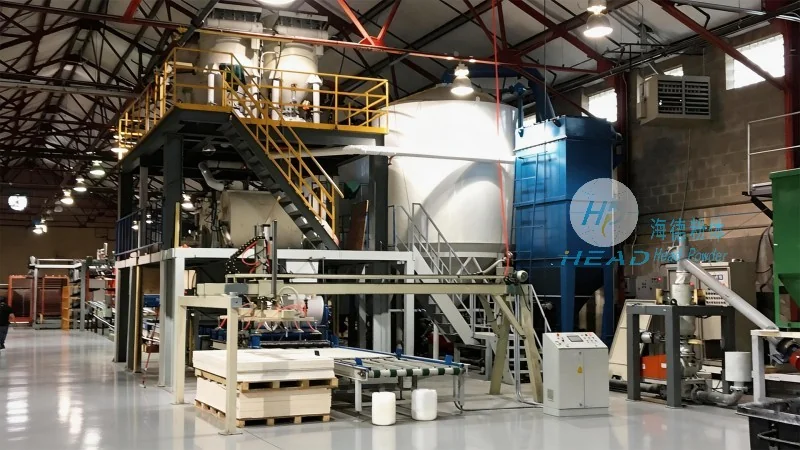
Operation Process: Step-by-Step Execution
The operation of the intelligent tonne bag feeding station material pneumatic conveying line follows a systematic sequence of steps. Initially, the tonne bag is placed on the receiving platform of the handling unit. The system then automatically lifts and positions the bag for processing. Next, the material opening mechanism activates, cutting open the bag and allowing the material to flow into the feeding hopper. The feeding mechanism then transfers the material from the hopper into the pneumatic conveying pipeline. The conveying system, driven by air compressors and control valves, moves the material through the pipeline to the processing equipment. Throughout the process, the control system continuously monitors parameters such as pressure, flow rate, and material level to ensure the system operates within safe and efficient parameters. Any deviations are immediately detected and corrected by the control system, preventing downtime and ensuring consistent material delivery.
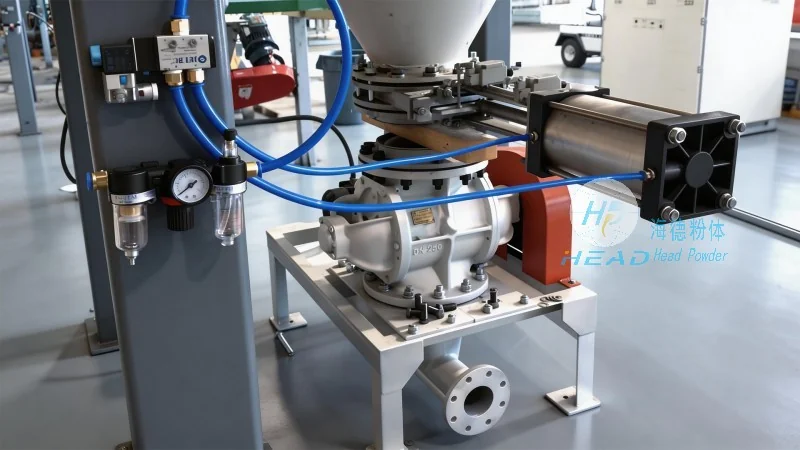
Working Principle: How the System Transfers Material
The working principle of the pneumatic conveying line is based on the movement of material particles within a gas stream. In this system, compressed air is used to create a flow that propels the material through the pipeline. The material is typically suspended in the air stream, which allows it to be transported over long distances and through various obstacles without the need for mechanical conveyors. The system may employ either positive pressure conveying, where air is forced into the pipeline carrying the material, or negative pressure conveying, where air is drawn out of the pipeline, creating a vacuum that pulls the material in. The choice of method depends on the material characteristics, such as particle size, density, and moisture content, as well as the distance and layout of the conveying line. The control system adjusts the air pressure and flow rate to optimize the conveying efficiency and minimize energy consumption.
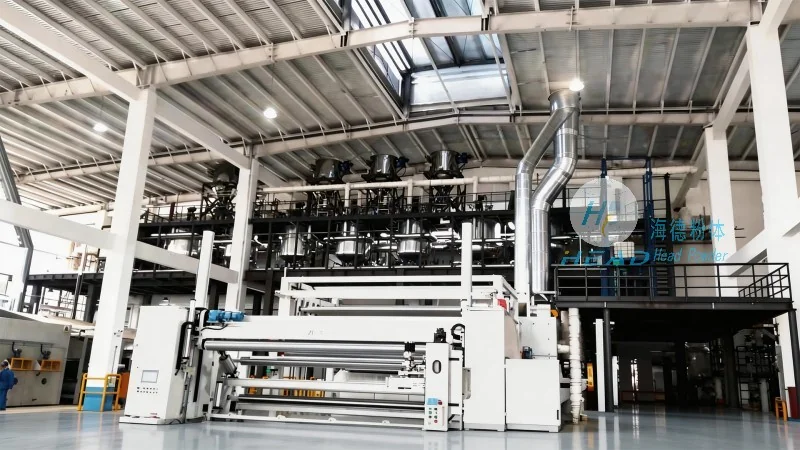
Advantages and Applications
The intelligent tonne bag feeding station material pneumatic conveying line offers several advantages over traditional material handling methods. It significantly reduces manual labor, minimizes material spillage and contamination, and improves operational safety by eliminating the need for workers to handle heavy or hazardous bags. The system also enhances process efficiency by providing a continuous and consistent material flow, which is crucial for maintaining production rates in industrial settings. This technology is widely applied in industries such as chemical, pharmaceutical, food, and mining, where bulk materials need to be handled with precision and reliability. The system's adaptability allows it to be customized to meet the specific requirements of different applications, ensuring optimal performance in diverse environments.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. has developed the intelligent tonne bag feeding station material pneumatic conveying line as a cutting-edge solution for modern material handling challenges. By integrating advanced automation and pneumatic conveying technologies, the system provides a reliable, efficient, and safe method for transferring bulk materials from tonne bags. With its comprehensive design and robust performance, this system is an essential asset for industries seeking to enhance their operational efficiency and maintain high standards of material handling. HeadPowder continues to innovate in this field, offering tailored solutions that meet the evolving needs of industrial applications.